

News
We'll get back to you as soon as possible.
How Do Industrial Corn Stalks Bio-RNG Projects Overcome Lignin Recalcitrance for Pipeline Injection?
Agricultural residues represent one of the most underutilized biological energy reservoirs globally. Among these, corn stover (comprising stalks, leaves, husks, and cobs) stands out due to its high carbon concentration and sheer abundance. Converting this fibrous residue into pipeline-quality renewable natural gas involves complex biochemical engineering and rigorous multi-stage gas upgrading. Industrial corn stalks bio-rng projects require precise system configuration to handle abrasive solids, disrupt recalcitrant cell structures, maintain biological equilibrium inside anaerobic digesters, and separate methane to concentrations exceeding 98%.
Overcoming Lignocellulosic Recalcitrance in Corn Stover
Corn stalks are composed of approximately 35% to 40% cellulose, 20% to 25% hemicellulose, and 15% to 20% lignin. The structural integrity of this biomass presents a formidable obstacle to hydrolytic microorganisms. Lignin forms a protective, non-fermentable phenylpropane sheath around the cellulose and hemicellulose fibers, severely restricting enzymatic accessibility during standard anaerobic conditions.
Raw stover also exhibits low bulk density and high hydrophobicity. When fed directly into wet digestion tanks without modification, the fibrous particles trap gas bubbles, float to the liquid surface, and generate thick crust layers that resist mechanical agitation. These characteristics demand specialized physical and thermal conditioning systems before entering fermentation vessels.
Mechanical and Extrusion Pretreatment Systems
Particle size reduction forms the baseline operational step for agricultural residues. Field-baled corn stover must first pass through high-torque stationary shredders and secondary hammer mills to bring fiber lengths below 10 millimeters. This mechanical shearing shatters the outer waxy cuticle, expanding the specific surface area available for enzymatic attachment.
Advanced facilities integrate mechanical twin-screw extrusion downstream of milling. The combination of sustained shear stress, internal pressure gradients, and controlled friction within the extruder barrel defibrillates the stover fibers. This process disrupts the crystalline structure of cellulose without producing toxic inhibitory byproducts like furfural or 5-hydroxymethylfurfural (5-HMF), which regularly occur when excessive thermal or acid-based methods are applied.
Hydrothermal and Steam Explosion Pathways
Larger corn stalks bio-rng projects frequently implement continuous hydrothermal conditioning or steam explosion to maximize the conversion rate of volatile solids. Processing corn stalks with saturated steam at temperatures between 160°C and 190°C under pressurized parameters (0.6 to 1.2 MPa) solubilizes the hemicellulose fraction into fermentable pentose sugars.
Rapid depressurization at the end of the hydrothermal cycle causes moisture within the plant cell walls to flash vaporize instantaneously. The resulting volumetric expansion tears apart the recalcitrant lignin matrix. This structural breakdown increases the ultimate biological methane potential (BMP) by 25% to 35% compared to untreated stalks, while cutting digestion retention times by half.
Anaerobic Digestion Architecture for Fibrous Biomass
Digestion of high-solids agricultural substrates behaves differently than municipal wastewater sludge or animal manures. Corn stalks feature a naturally high carbon-to-nitrogen (C:N) ratio, typically hovering between 45:1 and 60:1. The ideal metabolic operational window for methanogenic archaea lies between 20:1 and 30:1. Unadjusted mono-digestion of corn stover depletes available nitrogen swiftly, leading to volatile fatty acid (VFA) accumulation, dropping pH values, and complete acidogenesis stalling.
Co-Digestion Dynamics and Nutrient Balancing
Balancing nitrogen inputs requires continuous operational calibration. Many facilities implement co-digestion designs, blending prepared corn stalks with high-nitrogen liquid substrates such as swine slurry, dairy manure, or digestate centrate rich in ammonium. Where liquid manure logistics are constrained, industrial facilities introduce nitrogen chemicals like aqueous ammonia or urea alongside trace element cocktails containing nickel, cobalt, molybdenum, and selenium.
Trace minerals serve as catalytic cofactors for enzymatic complexes in the acetoclastic and hydrogenotrophic methanogenic pathways. Without routine supplementation, high-rate agricultural fermentation systems exhibit metabolic fatigue, marked by an accumulation of propionic and butyric acids that suppress the entire microbial community.
Digester Configuration: CSTR vs. High-Solids Plug Flow
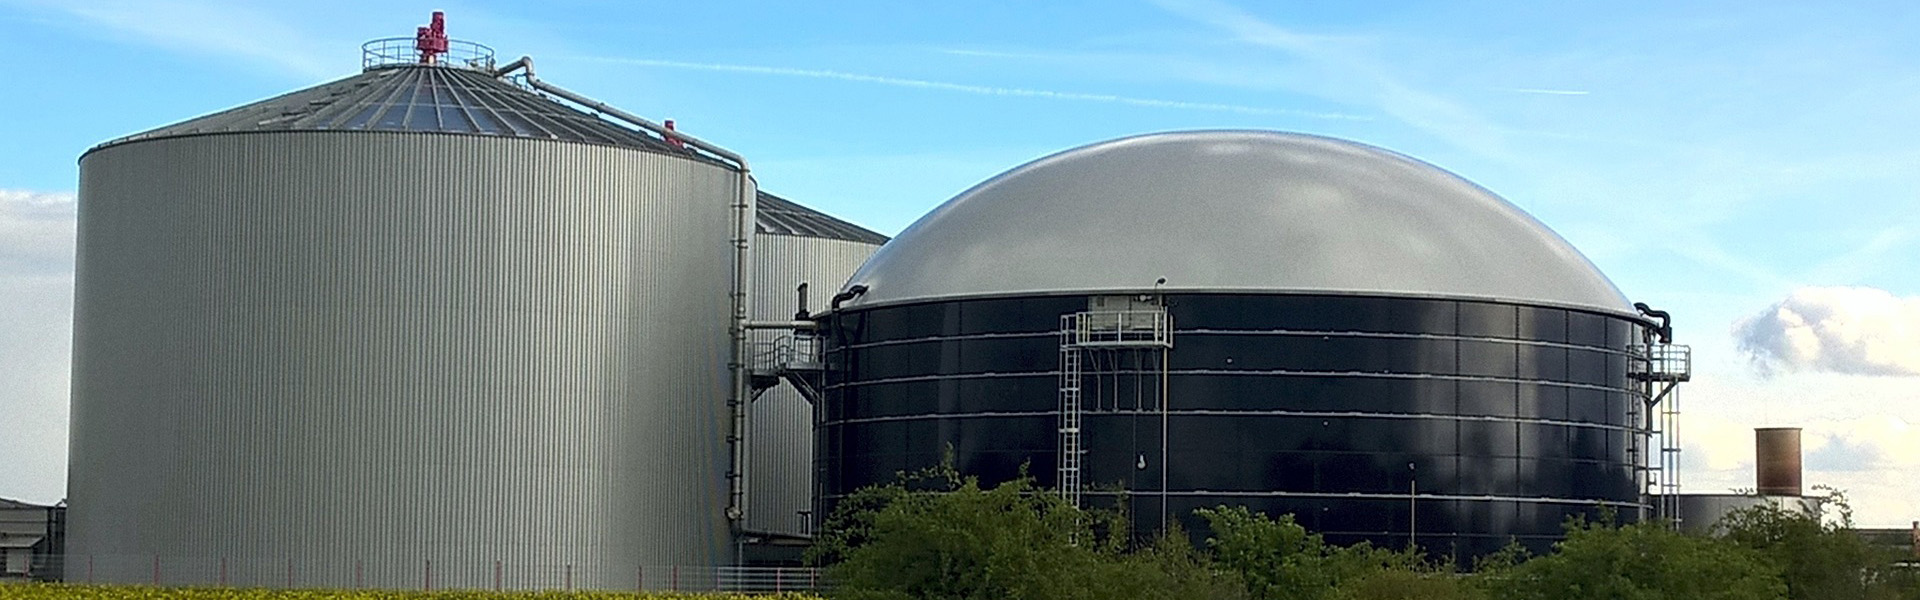
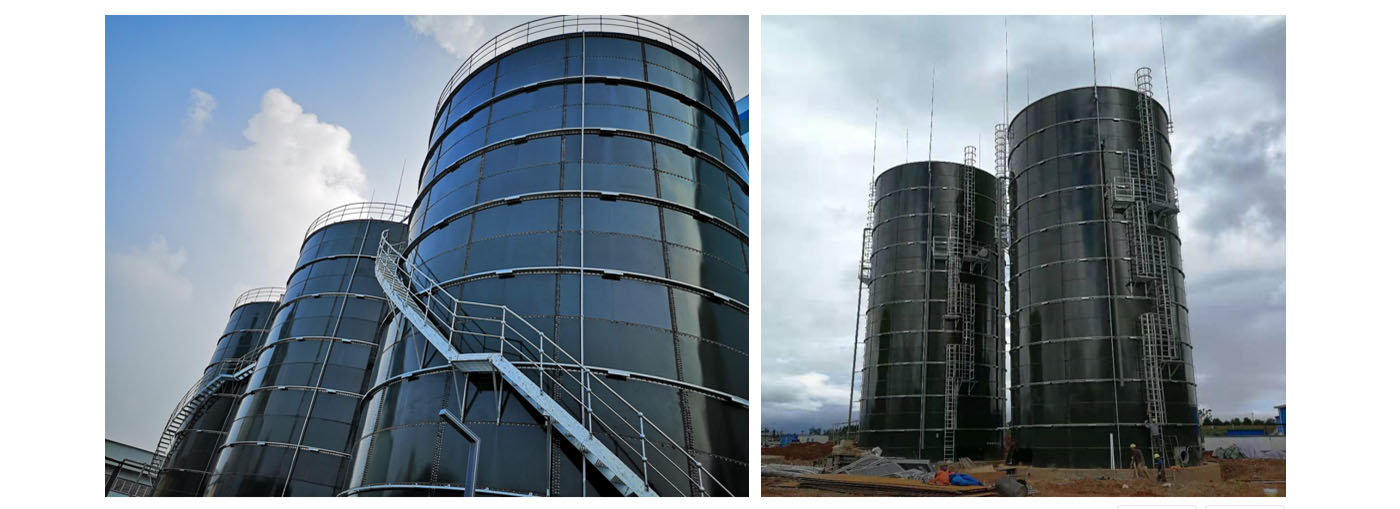
Selecting the digestion reactor format determines ongoing operational reliability. While traditional low-solids Continuous Stirred-Tank Reactors (CSTR) function adequately for dilute blends, dedicated corn stalks bio-rng projects favor specialized reactor architectures:
High-Solids Continuous Stirred-Tank Reactors: Reinforced digesters outfitted with high-torque, variable-depth vertical agitators or central draft-tube mixers capable of shearing floating fibrous mats before crust formation solidifies.
Horizontal Plug-Flow Digesters: Heavy-duty, slow-rotating horizontal shaft reactors designed specifically for total solids (TS) concentrations ranging from 15% to 22%. These systems move the viscous material uniformly from inlet to outlet, eliminating short-circuiting and dead zones.
Two-Phase Anaerobic Systems: Separation of hydrolytic/acidogenic processes in a primary reactor from methanogenesis in a secondary vessel. This operational split allows operators to maintain an acidic pH (5.5 to 6.2) in phase one to hydrolyze stover fibers quickly, while feeding the resulting organic acids into a precisely controlled, neutral-pH (7.2 to 7.8) second phase to produce high-concentration biogas.
Biogas Upgrading: Extracting Pipeline-Quality RNG
Biogas derived from corn stover digestion typically consists of 52% to 56% methane (CH4), 40% to 44% carbon dioxide (CO2), alongside variable contaminants including hydrogen sulfide (H2S, 500 to 2,500 ppm), moisture, trace nitrogen, oxygen, and siloxanes. Converting this wet, sour gas into pure renewable natural gas suitable for injection into commercial pipeline distribution networks requires aggressive purification equipment.
Bulk Desulfurization and Moisture Removal
Raw gas exiting the digester headspace passes immediately into biological or chemical desulfurization units. Coarse biological scrubbers rely on sulfur-oxidizing bacteria (such as Thiobacillus) to convert gaseous H2S into elemental sulfur in the presence of micro-dosed oxygen. To protect downstream membrane polymers or adsorption beds, secondary polishing vessels filled with iron sponge, extruded iron oxide pellets, or active carbon media drop residual H2S levels beneath 4 ppm.
Moisture knockout systems follow desulfurization. Direct chilling bundles depress the biogas temperature to 3°C to 5°C, causing bulk water vapor to condense and drain away. The cool gas then moves through deep-bed desiccant or molecular sieve dehydration towers, driving the operational dew point below -40°C.
Polyimide Hollow-Fiber Membrane Separation
Modern corn stalks bio-rng projects rely heavily on multi-stage hollow-fiber polyimide membrane systems for CO2 removal. These polymeric membranes operate based on differential gas permeability. Carbon dioxide, water vapor, and hydrogen sulfide possess high permeation rates through the polymer matrix, while methane permeates slowly, remaining on the high-pressure retentate side.
A typical three-stage membrane design works as follows:
First Stage: Compressed raw biogas (12 to 16 bar) enters the primary membrane modules. A high-purity biomethane stream exits as the retentate, while the permeate carries away a mix of CO2 and slip methane.
Second Stage: The permeate gas from the primary stage undergoes re-compression and treatment in a secondary membrane rack to recover methane slipped during initial separation.
Third Stage: The retentate from the secondary cycle is recirculated back into the primary inlet stream, while the final CO2-rich waste gas vents or flows into carbon capture systems, yielding an aggregate methane recovery rate above 99.2%.
Pressure Swing Adsorption and Amine Scrubbing
Adsorption and chemical scrubbing offer viable operational alternatives to membrane modules depending on site parameters:
Vacuum Pressure Swing Adsorption (VPSA): Multi-column systems packed with carbon molecular sieves (CMS). Gas components pass through the beds under high pressure where CO2 molecules are trapped within the microscopic pore structures while methane flows unhindered. Depressurization and vacuum extraction release the bound CO2 for cycle regeneration.
Chemical Amine Scrubbing: Systems using aqueous formulations of methyldiethanolamine (MDEA) or piperazine-activated solvents. Chemical absorption binds CO2 within an absorption tower via exothermic reactions. The solvent regenerates inside a stripping column through thermal steam reboiling. Amine systems deliver high methane purities (>99%) and minimal methane slip (<0.1%), though they consume substantial thermal energy during solvent regeneration.
Grid Injection Compliance and Process Control
Biomethane derived from agricultural residues must satisfy strict pipeline interconnect standards before transmission system operators permit custody transfer. Ensuring continuous regulatory compliance requires real-time gas chromatography and safety bypass manifolds.
Off-Spec Diversion Systems and Analytical Monitoring
Fast-response process gas chromatographs analyze the dry gas stream continuously, measuring methane content, gross heating value, Wobbe Index, oxygen concentrations, carbon dioxide levels, and residual moisture. If any parameter drifts outside pre-set pipeline tolerances—such as oxygen exceeding 10 ppm or total inerts surpassing 3%—automated fast-acting fail-safe valves immediately close the pipeline entry valve and reroute the biomethane stream to the flare stack or back to the digester gas holder until the upgrading train recalibrates.
Compressor sets, typically multi-stage reciprocating or oil-free screw compressors, then elevate the accepted biomethane from upgrading pressures (around 10 to 15 bar) to the required grid transmission level, which often spans 40 to 80 bar.
Digestate Processing and Nutrient Recovery
A full-scale agricultural project processing 50,000 to 100,000 tons of corn stalks annually yields vast volumes of whole digestate. This byproduct retains all the nitrogen, phosphorus, and potassium inputs, alongside undigested lignin and microbial biomass.
Mechanical solid-liquid separation via continuous decanter centrifuges or screw presses splits the digestate into two distinct revenue streams:
Solid Fraction: High-dry-matter cake (25% to 35% TS) containing fibrous matter and organic phosphorus. This material can be composted into soil amendments or dried and used as animal bedding.
Liquid Centrate: A nutrient-rich stream containing soluble ammoniacal nitrogen and potassium. A portion of this liquid recirculates to the front of the plant to hydrate incoming shredded corn stover, closing the process water loop, while the remaining balance goes to seasonal field application via low-emission trailing-shoe or direct-injection tankers.
Material Handling and Plant Wear Engineering
Corn stalks harvested from industrial crop fields bring severe physical challenges: high silica dirt contamination, stones, tramp metal, and naturally abrasive fibers. System engineers must specify robust materials across all substrate handling systems to prevent frequent unscheduled plant shutdowns.
Feeding bins require integrated destoning basins and overhead cross-belt neodymium magnets to strip away ferrous scrap before mechanical shredding begins. Slurry transport pipes should consist of high-density polyethylene (PE100) or thick-walled ceramic-lined steel at high-wear directional elbows. Progressive cavity pumps and rotary lobe pumps handling chopped stover mixtures must feature tungsten carbide coating on rotating components and adjustable elastomer stators to counteract continuous abrasion.
Implementing programmable reverse-rotation sequences on mechanical mixers protects impellers from long, flexible fibers that can wrap around driveshafts, stall motors, and burn out gearboxes.
Commercial Execution of Stover Biomethane Plants
Executing successful corn stalks bio-rng projects demands complete continuity between agricultural harvesting schedules, raw stover storage preservation, high-efficiency mechanical pretreatment, balanced biochemical conversion, and exact gas processing. By tailoring equipment selection to the physical realities of lignocellulosic material, project developers can convert abundant crop residues into pipeline-ready energy assets.
If you are planning an agricultural gas conversion facility or require rugged, skid-mounted biogas upgrading systems designed specifically for agricultural crop residues, submit a project inquiry to our engineering team today. Our technical specialists evaluate feedstocks, specify high-durability digestion and purification systems, and deliver fully integrated processing solutions tailored to your regional injection requirements.
Frequently Asked Questions
Q1: What methane yield can operators realistically expect from processed corn stalks?
A1: Methane yield depends heavily on the thoroughness of mechanical preparation and biological retention periods. Well-conditioned corn stover with moisture levels under 15% typically delivers a biological methane potential ranging from 220 to 290 normal cubic meters (Nm³) of methane per ton of volatile solids (VS). Without upstream physical or thermal disruption of the lignin matrix, practical yields regularly fall below 180 Nm³/ton VS.
Q2: How does silica and field soil contamination impact downstream gas upgrading equipment?
A2: Soil, sand, and grit collected during harvesting settle out inside digester tanks, reducing active volume over time. If carried through the slurry circuit, these fine silicates erode pump impellers and progressive cavity stators. However, silica does not volatilize into the gas phase; it remains in the liquid digestate. Biogas cleaning components such as membranes and carbon beds remain unaffected by mineral sand, provided effective aerosol and moisture separation is maintained upstream.
Q3: Why is continuous trace element dosing required when digesting corn stover?
A3: Corn stover is fundamentally a structural carbohydrate source rich in carbon, but poor in micro-nutrients. Methanogenic microorganisms require catalytic metals, particularly nickel, cobalt, and molybdenum, to synthesize enzymes for metabolic pathways like methyl-coenzyme M reductase. In mono-digestion scenarios, lack of trace metals limits microbial populations, resulting in elevated volatile fatty acid levels and dropped conversion efficiency.
Q4: What happens to the high volumes of carbon dioxide removed during the upgrading phase?
A4: The high-pressure CO2 stream isolated by hollow-fiber membranes or amine stripping towers can follow two routes. Facilities without recovery infrastructure discharge this biogenic CO2 through a high-level exhaust silencer. Increasingly, modern installations install liquefaction modules to purify, chill, and liquefy the offgas into food-grade liquid carbon dioxide (purity >99.9%), turning a waste stream into a salable industrial chemical.
Q5: Can corn stalks be fed into the digester year-round despite single-season harvesting?
A5: Yes. Year-round operation requires structured field logistics and storage management. Corn stover collected in autumn is either baled at low moisture (<15%) and stored under protective tarpaulins or wrapped tubes, or chopped green and compacted into silage bunkers. Silage preservation initiates lactic acid fermentation that preserves organic material over 12 months with negligible dry matter degradation, securing stable feed for continuous biomethane output.